 Joseph Robertson
ef3c47135f
Follow-up to #16195 and the review discussion on #14394 (yw4z's note
about the third column on the *Belt tilt* row). Removes the belt options
that are redundant or unused before the branch ships, so they never need
compatibility handling after a release, and fixes supports under a
leading overhang. Every removed key is on `handle_legacy()`'s ignore
list, so existing profiles and 3MFs load silently.

## Removed

- **`belt_slice_rotation_global`**, **`preslice_remap_global`**,
**`belt_preslice_global`** (*Global mesh transforms*) and
**`gcode_back_transform`** — the global mode and the back-transform are
what belt printing is; they are presumed on wherever the flags were
consulted (`PrintObjectSlice`, `BeltBackTransform`, `BeltGCode`,
`Print::process`, `PrintApply`, `GCodeViewer`). The *Belt tilt* row is
axis + angle only; the three `fdm_belt_common.json` drop the keys.
- **`preslice_remap_x/y/z`** — no profile used the pre-slice axis remap;
the belt tilt axis plus the G-code axis remap cover the machines that
exist, and its implementation only agreed with itself for a plain swap.
The forward transform is the rotation.
- **`belt_support_z_offset_mode`** and **`belt_support_floor_mode`** —
the first was never read by a generator; the second's only shipped value
(*Generator only*) is now the behaviour.
- **`first_layer_plane`**, **`first_layer_plane_offset`**,
**`first_layer_plane_thickness`** and `FirstLayerPlane.{cpp,hpp}` — the
first-layer band is measured from the belt surface and is one first
layer height thick.
- `belt_brim_instances_compatible()` and its validation warning:
instances along the belt get their brim.

## Supports under a leading overhang (the clipping at the object's local
Z = 0)

The slicing frame of a belt object started at its lowest vertex, but the
belt under the leading end of an overhang lies below that, so no
generator could reach it: normal supports stopped at the object's lowest
layer, and both tree generators carried extension hacks sized from the
pre-rotation bbox and capped at global Z = 0 (right only for the
trailing half of the belt). The frame now starts at the lowest
belt-floor point under the footprint, less a 10 mm margin along the belt
for the base of a support column, and the extensions are gone:

- **Normal supports** run in the object frame and get the global belt Z
offset shifted onto the result (as organic already did). With the offset
on the object layers, a top contact at negative Z turned the
intermediate-layer count negative and the generator allocated layers
until the kernel killed it — any overhang in the leading half of the
belt did this. The first-layer flange expansion is skipped on a belt
(the first support layer is the leading tip, not a flange).
- **Classic tree** nodes keep dropping until their whole circle is in
the belt, so a branch tapers to a tip on the belt instead of stopping a
radius above it.
- **Organic**: the belt is no longer a support blocker. A blocker is a
collision, and a branch descending onto one slides off it, down the belt
and ahead of the part; the belt is where branches end, which the
per-layer floor clipping already does.

Regression test *Belt supports reach the belt under a leading overhang*:
a cube with a fin whose underside is parallel to the layers, 20 mm ahead
of the cube and up to 41 mm of slicing Z above the belt, for normal,
organic and classic tree supports; the lowest support layer must sit on
the belt beneath its own lines.

The belt object height (the layer range) is now estimated from the box
of the mesh as placed on the bed. `raw_bounding_box()` has the
instance's Z offset removed, which was harmless for the old
rotated-extent estimate but not for one anchored at the belt floor (a
point's rotated z and the floor under it move in opposite directions
under a Z shift): with the first version of this change every part came
out as a wedge, sliced only up to its diagonal, in the GUI and CLI
alike. Caught by a GUI test pass; the leading-overhang test now also
checks that the whole part is sliced.

## Belt brim after the parallel support step

`belt_brim_obstacles()` reads every object's layers and support layers,
which another object's support step rebuilds (and now shifts) at the
same time. The brim is generated sequentially once the parallel step is
over (`PrintObject::generate_belt_brim()`). This is the race behind the
Windows arm64 segfault in *Belt brim of each object precedes its
perimeters on its own filament*.

## UI

- *Belt tilt* is two rows: the angle (Advanced) and the axis (Developer;
a profile-level kinematics choice). A shared line is shown by its first
option's mode, so they cannot share one.
- *Machine frame transforms* is five single-option rows (G-code remap X
/ Y / Z, Decouple machine-frame tilt, Machine-frame tilt angle — the
angle row only appears when decoupled) instead of two multi-column
lines; the remap fields got full labels since they stand alone now.
- The gravity indicator on the bed is a plain line along the up
direction (no cone, 60 % of the axes' length), per yw4z.
- The *Show raw G-code (belt only)* legend/canvas toggle and its `B`
shortcut are gone; the preview is the designed view.

Also carries the two-line `phong.fs` fix from #16226 (merges as a
no-op).

## Verification

- `libslic3r_tests` 1116 passed (92 648 assertions); `fff_print_tests`
351 passed (561 696 assertions).
- `scripts/clang_tidy_diff.py --base upstream/belt-printer`: no
findings.
- `scripts/orca_profile_tool.py check`: no profile references a removed
key.
- GUI target builds; a scripted GUI pass (xdotool) checked the settings
groups in every mode, slicing, export, instances, the purge tower,
calibration dialogs, the wizard, printer switching and 3MF round-trip.

The wiki pages (OrcaSlicer/OrcaSlicer_WIKI#374) get a follow-up dropping
the removed sections once this is in.


OrcaSlicer: an open source Next-Gen Slicing Software for Precision 3D Prints.
Optimize your prints with ultra-fast slicing, intelligent support generation, and seamless printer compatibility—engineered for perfection.
Official links and community
Official Website:
Github Repository:

Follow us:


Join our Discord community:

|
⚠️ CAUTION: Several clickbait and malicious websites, such as orca-slicer[.]com and orcaslicer[.]net, are pretending to be the official OrcaSlicer site. These sites may redirect you to dangerous downloads or contain misleading information. Our only official website is www.orcaslicer.com. If you come across any of these in search results, please report them as unsafe or phishing to help keep the community secure with: - Google Safe Browsing - Microsoft Security Intelligence - IPThreat |
Main features
- Advanced Calibration Tools
Comprehensive suite: temperature towers, flow rate, retraction & more for optimal performance. - Precise Wall and Seam Control
Adjust outer wall spacing and apply scarf seams to enhance print accuracy. - Sandwich Mode and Polyholes Support
Use varied infill patterns and accurate hole shapes for improved clarity. - Overhang and Support Optimization
Modify geometry for printable overhangs with precise support placement. - Granular Controls and Customization
Fine-tune print speed, layer height, pressure, and temperature with precision. - Network Printer Support
Seamless integration with Klipper, PrusaLink, and OctoPrint for remote control. - Mouse Ear Brims & Adaptive Bed Mesh
Automatic brims and adaptive mesh calibration ensure consistent adhesion. - User-Friendly Interface
Intuitive drag-and-drop design with pre-made profiles for popular printers. - Open-Source & Community Driven
Regular updates fueled by continuous community contributions. - Wide Printer Compatibility
Supports a broad range of printers: Bambu Lab, Prusa, Creality, Voron, and more. - Additional features can be found in the change notes.
Wiki
The wiki aims to provide a detailed explanation of the slicer settings, including how to maximize their use and how to calibrate and set up your printer.
Download
Stable Release
📥 Download the Latest Stable Release
Visit our GitHub Releases page for the latest stable version of OrcaSlicer, recommended for most users.
Nightly Builds
🌙 Download the Latest Nightly Build
Explore the latest developments in OrcaSlicer with our nightly builds. Feedback on these versions is highly appreciated.
Belt Printer Builds
The nightly release ships two parallel builds: the standard build and a belt-printer build. Both are attached to the same release — tell them apart by the filename suffix:
- Standard — no suffix (e.g.
OrcaSlicer_Windows_Installer_x64_nightly.exe) - Belt —
_beltsuffix (e.g.OrcaSlicer_Windows_Installer_x64_nightly_belt.exe)
The _belt builds add experimental support for belt / conveyor (infinite-Z) printers, where the model is sliced against a tilted belt surface instead of a flat horizontal bed. They include ready-to-use belt printer profiles, the full belt slicing pipeline (mesh rotation and G-code transforms), belt-aware support generation, and a tilted-bed preview.
⚠️ Belt printer support is under active development and is not yet merged into
main— it currently ships only in these parallel_beltbuilds, produced from thebelt-printerbranch. See tracking PR #14394 and the original documentation in #12998.
How to install
Windows
Download the Windows Installer exe for your preferred version from the releases page. Both x64 and arm64 installers are published — pick the one matching your CPU.
-
For convenience there is also a portable build available.
Troubleshooting
- If you have troubles to run the build, you might need to install following runtimes:
- MicrosoftEdgeWebView2RuntimeInstallerX64
- vcredist2019_x64
- Alternative Download Link Hosted by Microsoft
- This file may already be available on your computer if you've installed visual studio. Check the following location:
%VCINSTALLDIR%Redist\MSVC\v142
Microsoft Store
Install from the Microsoft Store when you prefer a Store-signed package (helps on Windows 11 Smart App Control).
Windows Package Manager
winget install --id=SoftFever.OrcaSlicer -e
Mac
-
Download the universal DMG, which runs on both Apple Silicon and Intel Macs.
-
Drag OrcaSlicer.app to Application folder.
-
If you want to run a build from a PR, you also need to follow the instructions below:
Quarantine
-
Option 1 (You only need to do this once. After that the app can be opened normally.):
- Step 1: Hold cmd and right click the app, from the context menu choose Open.
- Step 2: A warning window will pop up, click Open
-
Option 2: Execute this command in terminal:
xattr -dr com.apple.quarantine /Applications/OrcaSlicer.app -
Option 3:
- Step 1: open the app, a warning window will pop up

- Step 2: in
System Settings->Privacy & Security, clickOpen Anyway:
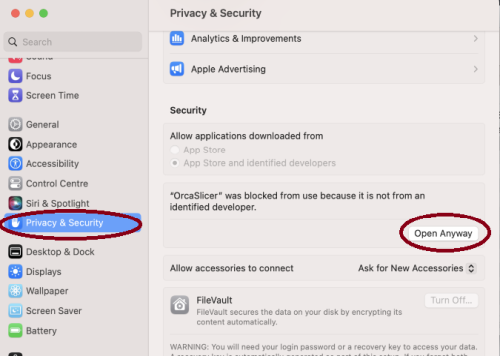
- Step 1: open the app, a warning window will pop up
-


Homebrew Cask
brew install --cask orcaslicer
The Homebrew cask installs the official macOS DMG from GitHub Releases.
Linux
Flathub (Recommended)
OrcaSlicer is available through FlatHub:
Install from the command line:
flatpak install flathub com.orcaslicer.OrcaSlicer
flatpak run com.orcaslicer.OrcaSlicer
It can also be installed through graphical software managers (KDE Discover, GNOME Software, etc.) when Flathub is enabled. Search for OrcaSlicer in your software center.
AppImage
AppImages are published for both x86_64 and aarch64 (ARM64). Pick the file matching your CPU — the ARM64 build has aarch64 in its name (e.g. OrcaSlicer_Linux_AppImage_Ubuntu2404_aarch64_*.AppImage).
-
Download App image from the releases page.
-
Double click the downloaded file to run it.
-
If you run into trouble executing it, try this command in the terminal:
chmod +x /path_to_appimage/OrcaSlicer_Linux.AppImage
How to Compile
All updated build instructions for Windows, macOS, and Linux are now available on the official OrcaSlicer Wiki - How to build page.
Please refer to the wiki to ensure you're following the latest and most accurate steps for your platform.
Klipper Note
If you're running Klipper, it's recommended to add the following configuration to your printer.cfg file.
# Enable object exclusion
[exclude_object]

# Enable arcs support
[gcode_arcs]
resolution: 0.1
Supports
OrcaSlicer is an open-source project, and we're deeply grateful to all our sponsors and backers.
Their generous support helps fund filaments and other essential 3D printing materials for the project.
Thank you! :)
Sponsors

|

|
Backers:
Ko-fi supporters ☕: Backers list
Support the project


Some Background
Open-source slicing has always been built on a tradition of collaboration and attribution. Slic3r, created by Alessandro Ranellucci and the RepRap community, laid the foundation. PrusaSlicer by Prusa Research built on Slic3r and acknowledged that heritage. Bambu Studio in turn forked from PrusaSlicer, and SuperSlicer by @supermerill extended PrusaSlicer with community-driven enhancements. Each project carried the work of its predecessors forward, crediting those who came before.
OrcaSlicer began in that same spirit, drawing from BambuStudio, PrusaSlicer, and ideas inspired by CuraSlicer and SuperSlicer. But it has since grown far beyond its origins. Through relentless innovation — introducing advanced calibration tools, precise wall and seam control, tree supports, adaptive slicing, and hundreds of other features — OrcaSlicer has become the most widely used and actively developed open-source slicer in the 3D printing community. Many of its innovations have been adopted by other slicers, making it a driving force for the entire industry.
The OrcaSlicer logo was designed by community member Justin Levine.
License
- OrcaSlicer is licensed under the GNU Affero General Public License, version 3.
- The GNU Affero General Public License, version 3 ensures that if you use any part of this software in any way (even behind a web server), your software must be released under the same license.
- OrcaSlicer includes a pressure advance calibration pattern test adapted from Andrew Ellis' generator, which is licensed under GNU General Public License, version 3. Ellis' generator is itself adapted from a generator developed by Sineos for Marlin, which is licensed under GNU General Public License, version 3.
- The Bambu networking plugin is based on non-free libraries from BambuLab. It is optional to the OrcaSlicer and provides extended functionalities for Bambulab printer users.