* Add PlastAR and Printalot filament vendors

Two Argentine brands from Printalot: PlastAR (budget PLA) and Printalot
(ABS). Each has a tuned @base plus per-color presets covering the
manufacturer's color lineup.

PlastAR PLA: flow 0.98, 1.75 mm, nozzle 220 C (190-230), bed 60 C; 14 colors.
Printalot ABS: flow 0.94, density 1.05, retraction 0.2 mm, max volumetric
18 mm3/s, nozzle 250 C (240-270), bed 100 C; 14 colors.

Per-color presets inherit their @base (no per-color parameter changes).
Passes scripts/orca_extra_profile_check.py.

* Ship PlastAR and Printalot as a single Printalot filament vendor

Place both Argentine lines in one OrcaFilamentLibrary/Printalot bundle and follow the library's brand shape: a non-selectable @base plus one all-printer @System per product, which is where a library preset meant for every printer belongs. The former per-color presets are dropped, leaving PlastAR PLA and Printalot ABS with their PLA and 250 C ABS material values. setting_ids are minted by the tooling; filament_ids resolve through the @base roots.

---------

Co-authored-by: SoftFever <103989404+SoftFever@users.noreply.github.com>
Co-authored-by: SoftFever <softfeverever@gmail.com>
* Add Polymaker PLA Pro filament profile

Polymaker PLA Pro is present in the tree only as printer-scoped variants
under Snapmaker U1 and Anycubic Kobra S1, so it is invisible to every other
printer. This adds it to the Orca Filament Library as OGFPM020 so it is
selectable generally.

Values are taken from the manufacturer's published print settings and
cross-checked against the two existing vendor profiles:

  density 1.23 g/cm3       both existing profiles agree
  softening 55 C           both existing profiles agree
  nozzle 220 C (210-230)   manufacturer's stated range
  max volumetric speed 15  Snapmaker 15, Anycubic 16

Flow ratio is set to 0.96, matching the Snapmaker profile. Worth noting for
review: the two existing profiles disagree here -- Snapmaker 0.96, Anycubic
0.85 -- because flow ratio depends on the extruder as much as the filament.
Any single value in a vendor-neutral preset is a starting point users should
calibrate; 0.96 is closer to the generic PLA baseline than 0.85 is.

setting_id assigned by scripts/assign_vendor_setting_ids.py.
OrcaFilamentLibrary version bumped 02.04.00.03 -> 02.04.00.04.

* fix errors

---------

Co-authored-by: SoftFever <103989404+SoftFever@users.noreply.github.com>
Co-authored-by: SoftFever <softfeverever@gmail.com>
* Add Meltingplot vendor profiles (CHX 350 + MBL series)

Adds the Meltingplot vendor bundle with 5 printer models:
- CHX 350 (880x422x943, RepRapFirmware/Duet)
- MBL 133/136/308/480 (RepRapFirmware/Duet)

Each model ships 0.4/0.6/0.8/1.0/1.2 nozzle variants. Layer height
presets span 40-60% of the nozzle diameter and deliberately avoid
heights that divide the Z screw lead evenly (CHX: 1204 ball screw,
4 mm lead; MBL: TR4x2 trapezoidal screw, 8 mm lead) so periodic
screw error does not repeat as banding.

All printers use 2.85 mm filament, so the bundle carries its own
filament library (PLA, StoneFil, ABS, TitanX, ASA, PETG, PA6 CF HT,
STYX 12, PP 9-2, PET-CF15, Extrudr PLA NX2 Matt, Igus iglidur J260)
with the 2.85 mm diameter pinned once in the vendor-local
fdm_filament_common base.

Machine limits mirror the printers' firmware configuration; machine
limit emission is disabled so the values only feed the time estimator.

* Add per-nozzle volumetric flow limits and nozzle size in filename

Cap filament volumetric speed per nozzle (0.4: 14, 0.6: 20, 0.8: 26,
1.0: 30, 1.2: 40 mm3/s). Filaments whose limit exceeds a nozzle's
capability get a nozzle-scoped child profile that only lowers
filament_max_volumetric_speed; filament_id is inherited so all nozzle
variants remain the same material.

Also include layer height and nozzle diameter in the g-code filename.

* Set CHX 350 machine time cost to 5 EUR/h

* Inherit Meltingplot filaments from OrcaFilamentLibrary generics

Per the profile creation guide, vendor filament profiles now inherit
from Generic * @System instead of vendor-local fdm_filament_* copies.
Each profile carries only Meltingplot-specific deviations plus the
2.85 mm filament diameter; the seven local fdm_filament_* base files
are removed.

Deliberate pins where the library default would change tuned behavior:
- PLA/ABS/TitanX keep filament_max_volumetric_speed 20 (0.6 nozzle cap)
- ABS/PET-CF15 keep close_fan_the_first_x_layers 1
- STYX 12 sets required_nozzle_HRC 0 (unfilled PA12, density 1.02)

* Remove Meltingplot StoneFil filament profile

* Meltingplot ABS: use library fan settings

* Meltingplot TitanX/ABS: use library fan and nozzle temperature settings

* Remove STYX 12, PP 9-2 and Igus iglidur J260 filament profiles

* Meltingplot ASA: use library fan_max_speed

* Derive per-nozzle volumetric speed caps from physical limit formula

Caps now follow V = 34*d * m / S: the 34*d limit line calibrated on
Micro Swiss Volcano plated copper at 2.85 mm, material factor m from
the OrcaFilamentLibrary generic ratios (PLA/ABS/ASA 1.0, PETG 10/12,
PETG-CF 11.5/12, PA-CF 8/12, PLA Matte 11/12), safety factor S = 1.25
covering batch/moisture/wear/diameter tolerances.

Each material base now serves the 1.2 nozzle at its maximum cap;
children @0.4-@1.0 lower the cap per nozzle. Machine variant
default_filament_profile entries point at the matching preset.

* Scale slow_down_layer_time per nozzle from bead cross-section

Minimum layer time follows the derived cooling rule: heat per layer
scales with bead cross-section (layer height x line width), so the
0.8-nozzle-tuned values are scaled by q(d)/q(0.8) using each nozzle's
standard preset geometry. Bases carry the 1.2 value, children @0.4-@1.0
their nozzle-specific value.

* Meltingplot: lift Z above the print before the end macro

Add a G90 / G1 Z{min(max_layer_z + 5, printable_height)} F600 move at the
start of machine_end_gcode, before M98 print_end shuts the printer down and
parks it. Besides clearing the part, the explicit Z coordinate lets the Duet
file-info parser pick up the object height.

* Meltingplot: cap default layer height at 40% of outer wall width

A 45 deg slope shifts each bead outward by exactly one layer height. With
the Slic3r bead model (rectangle (w-h) x h plus half-circles of diameter h)
the flat contact band to the layer below is w - 2h, so the maximum
self-supporting angle is atan((w-h)/h). Support cannot compensate: the
stair tread at 45 deg is only h wide, far below one support line width, so
no support line ever fits underneath a single step.

All ten machine variants defaulted to h/w = 0.455..0.524, i.e. at or past
the h/w = 0.5 point where the flat contact vanishes. The 0.8 nozzle default
(0.44 mm at w = 0.84) reached atan(0.4/0.44) = 42.3 deg and failed on 45 deg
slopes even with support.

Default presets now satisfy h <= 0.40 * outer_wall_line_width, which leaves
one third of the bead's flat underside in contact at 45 deg and puts the
geometric limit at 56.3 deg. To keep the defaults on sensible ladder rungs,
outer wall width is widened where it was the binding constraint:
chx_small 110 -> 115%, chx_large 105 -> 110%, mbl_04 105 -> 115%.

Ladders are unchanged; the thicker rungs stay available for parts without
steep overhangs.

* Meltingplot PLA: raise slow_down_layer_time by calibration factor 1.5

Print feedback on CHX 350 with a 0.8 nozzle at 0.44 mm layer height showed
curling at the retraction points with the derived value of 25 s. There is no
cooling headroom left to trade: fdm_filament_pla pins fan_min_speed =
fan_max_speed = 100, and additional_cooling_fan_speed is inert because no
Meltingplot machine enables auxiliary_fan. Minimum layer time is the only
remaining lever; 35 s prints cleanly at that geometry.

The cross-section rule only fixes the ratios between nozzle sizes, so this
is a calibration of the PLA anchor itself: both PLA ladders are scaled by
1.5 (Extrudr 9/20/38/56/83 s, Meltingplot PLA 8/17/30/45/66 s for
0.4/0.6/0.8/1.0/1.2). The Extrudr base fan_cooling_layer_time goes 60 -> 100
so the 1.2-nozzle value stays below it.

Other materials are left unchanged - only the PLA anchor has a real
counter-example so far.

* Meltingplot: drop layer heights that cannot print 45 degree walls

A preset whose layer height exceeds ~45% of the outer wall line width has
less than ~6 degrees of reserve on a 45 degree wall (max self-supporting
angle atan((w-h)/h)), and support cannot compensate because the 45 degree
stair tread is only h wide - far below one support line. Those presets are
not usable in practice, so shipping them only invites failed prints.

Removes the 22 rungs above h/w = 0.45 and prunes them from the vendor
index. What remains per nozzle (default first):

  CHX 350   0.4: 0.18 | 0.6: 0.24 0.28 | 0.8: 0.32 0.36
            1.0: 0.44 0.48 | 1.2: 0.48 0.56
  MBL       0.4: 0.18 | 0.6: 0.24 0.28 | 0.8: 0.36 0.34
            1.0: 0.44 0.48 | 1.2: 0.48 0.56

The 0.4 nozzle keeps a single rung: 0.20 mm would qualify (h/w = 0.435) but
divides both screw leads evenly (4/0.20, 8/0.20) and stays excluded by the
Z-artifact rule, and 0.22 is already at 0.478.

Also corrects the MBL 0.8 default to 0.36 mm, which at w = 0.92 sits at
h/w = 0.391 and therefore still satisfies the stricter 40% default rule.

* Meltingplot: require 5 degrees of reserve on 45 degree walls

Replaces the two separate thresholds (h <= 0.40 * outer wall width for
defaults, 0.45 for ladder rungs) with a single requirement stated on the
design constraint itself: every shipped preset must reach

  a_max = atan((w - h) / h) >= 50 deg

i.e. 5 degrees of reserve on a 45 degree wall, equivalent to
h <= 0.456 * outer_wall_line_width. The default is simply the thickest rung
that passes.

The 11 degrees the 40% rule produced were more margin than the failure mode
warrants, and cost throughput for no return. For calibration: across 940
machine defaults from 60 vendor bundles in this repo, the median reserve is
+1.8 deg, 71% ship less than 5 deg, and 8% cannot geometrically produce a
45 deg wall at all.

Adds the rungs the relaxed threshold makes available - 0.30 (0.6 nozzle,
both series) and 0.38 (0.8 nozzle, both series) - and restores the 0.30 mm
MBL preset removed in 5b4862b3 with its original setting_id. 0.20 mm on the
0.4 nozzle and 0.50 mm on the 1.0 nozzle would also qualify but stay
excluded because they divide both screw leads evenly.

Defaults are now (0.4/0.6/0.8/1.0/1.2) 0.18/0.30/0.38/0.48/0.56 for both
series, at 50.2 to 57.3 deg. The 1.2 nozzle deliberately keeps 0.56 rather
than the 0.60 the rule would allow: solidification time scales with h^2 and
bead weight with h*w, so the largest nozzle is the one that should not sit
on the minimum.

* Meltingplot: disable precise wall by default

Precise wall was inheriting OrcaSlicer's global default of true. Disable it
bundle-wide in the vendor process root so it applies to CHX 350 and all MBL
models. Note it was already ignored on the CHX small-nozzle branch, which
uses the inner-outer-inner wall sequence.

* Meltingplot CHX: raise max extruding acceleration to 6000

The 4000 limit silently clamped the profiles' 6000 values for default and
inner wall acceleration, since GCodeWriter caps print acceleration against
machine_max_acceleration_extruding regardless of emit_machine_limits_to_gcode.
Raising it to 6000 matches the X/Y limits so the configured values are emitted
as-is. The firmware's own M201 still governs what is actually driven.

* Meltingplot PA6 CF HT: raise part cooling floor to 40%

Sharp 90 degree corners were washing out layer by layer while straight walls
and overhangs printed cleanly. Overhangs are fine because overhang_fan_speed
forces 100% regardless of layer time; everything else fell back to
fan_min_speed, since at the layer times seen in practice neither branch of the
layer-time fan interpolation applies.

Raise fan_min_speed to 40% and set reduce_fan_stop_start_freq so that floor is
actually applied instead of dropping to zero. Also lower the auxiliary fan to
40% and raise the overhang cooling threshold to 95%, matching the values
validated on the print.

* Meltingplot: re-mint filament ids with orca_id_tool

Upstream now requires every filament_id to be a minted "OF" id derived
from the (filament_vendor, filament_type, name) triple and recorded in
scripts/filament_id_snapshot.json. The hand-made ids this bundle shipped
with (MPFPLA0, EXTNX2M, ...) were rejected by orca_extra_profile_check.

Regenerate them with "orca_id_tool.py --generate --vendor Meltingplot"
and record the result with --update-snapshot. No setting_id changed, and
the ids were never released, so no existing project file refers to them.

* Meltingplot: normalize bundle for updated profile checks

Drop obsolete keys (silent_mode, adaptive_layer_height, tree_support_with_infill) and rebuild the vendor index in canonical order, as orca_profile_tool.py normalize / update-index write them.

* Meltingplot: list per-nozzle filaments in default_materials

The unsuffixed filament presets only cover the 1.2 mm variants, so the 0.4-1.0 mm printer presets had no compatible entry in their model's default_materials. The validator's check_printer_default_materials rejects that, and load_installed_filaments would auto-install no filament for those variants on first run. Name the @0.4/0.6/0.8/1.0 nozzle presets alongside the base ones for PLA, PETG, ABS and ASA.

---------

Co-authored-by: yw4z <ywsyildiz@gmail.com>
* Add Flashforge Adventurer A5 printer profiles

Adds system profiles for the Flashforge Adventurer A5 to the existing
Flashforge vendor: the machine model with 0.25/0.4/0.6/0.8 mm nozzle variants,
14 process presets, and 43 filament presets, plus the printer cover image.

All presets inherit from existing Flashforge bases already in-tree
(Adventurer 5M Pro nozzle profiles, AD5M Pro process/filament presets,
Flashforge generics); no new base assets are introduced (the A5 reuses the
existing 5M-series bed/hotend models and buildplate texture). Every inherits
reference and sub_path was validated to resolve.

Co-Authored-By: Claude Opus 4.8 (1M context) <noreply@anthropic.com>

* Assign setting_id to Adventurer A5 presets (fix profile check)

The new A5 filament and process presets were missing the deterministic
setting_id required by OrcaSlicer's profile validator. Generated via
scripts/assign_vendor_setting_ids.py (61 instantiated presets). Verified with
scripts/orca_extra_profile_check.py: 0 errors.

Co-Authored-By: Claude Opus 4.8 (1M context) <noreply@anthropic.com>

* Fix Flashforge Adventurer A5 profiles so the bundle loads and validates

The new A5 presets were not in canonical form, several filaments resolved
no or the wrong filament_id, and the model and machines pointed at
non-existent or AD5M Pro defaults. Run the standard profile tooling
(normalize, update-index, generate-id), give the branded filaments the ids
of their existing Flashforge products, and repoint the defaults at
A5-compatible filaments and processes. Bump the Flashforge bundle version.

---------

Co-authored-by: Claude Opus 4.8 (1M context) <noreply@anthropic.com>
Co-authored-by: yw4z <ywsyildiz@gmail.com>
Co-authored-by: SoftFever <103989404+SoftFever@users.noreply.github.com>
Co-authored-by: SoftFever <softfeverever@gmail.com>
* Add Ultimaker S5 Profile - WIP

* Add Ultimaker physical printer base

* Ultimaker API WIP for base update.

* Fix undefined reference error.

* Add UMS5 profile, add placeholders for testAuth stuff.

* Fix non-const func definitions, make func names align with style guide.

* Localization stuff? IDK if this does anything or is required.

* Add cover image

* Auth code cleanup, add UI button for auth cred generation, implement various auth checks and tests.

* Fix auth stuff

* Clean up code

* Get upload code sort-of working, fix typo

* Update printer settings and start/end gcodes

* Add makeGriffinCompatible preprocessor script to prevent machine crash, update machine profile.

* Fix buildplate size, fix time missing bug, add S5 buildplate model

* Correct capitalization to UltiMaker

* Fix display bug, fix capitalization bug

* Implement credential generation button and logic

* Fix generate auth creds button, add todos, fix capitalization.

* Actually fix generate auth credentials.

* Fix generate auth creds message.

* Update UM S5 machine limits

* Revert accidental commit.

* Fix postprocessor, clean up code.

* Update presets for multi-extruder printing.

* Add Single Extruder and Fast profiles.

* Code cleanup

* Register and validate the UltiMaker S5 presets

* Show the Generate API Key button only for UltiMaker print hosts

The PR added it to the Physical Printer dialog for every host type, where pressing it runs an ordinary connection test and reports "API Key created". Gate it on the selected host type instead.

* Drop unused lambda captures in the UltiMaker host code

clang promotes -Wunused-lambda-capture to an error under the project's -Werror, so the file failed to build on macOS; the five callbacks do not touch this.

* Fix the Windows build of the UltiMaker print host

---------

Co-authored-by: SoftFever <softfeverever@gmail.com>
* init

* drop usage of StaticGroup for ExtruderGroup

* completely remove StaticGroup from project

* fix alignment of "Not installed" text

* fix crash on linux while clicking edit button

* Fix background color on macOS

---------

Co-authored-by: Noisyfox <timemanager.rick@gmail.com>
Merged by /bot merge on behalf of @inslogic3d (id 321604763).
Grants: resources/profiles/OrcaFilamentLibrary/filament/INSLOGIC, resources/profiles/OrcaFilamentLibrary.json
Head: 22a51b32f0
# Description
Adds a sketch-first parametric CAD tab to the slicer: sketch → constrain
→ solid features
→ commit to plate. The feature recipe is persisted inside the 3MF, so
reopening a project
restores an editable model rather than a frozen mesh.
Opening this at @SoftFever's request, so the code is easier to read than
a fork.
**The number worth reading first:** the diff is large, but almost all of
it is new files.
Existing upstream code is touched in **23 files, +622 / -88 total**.
That is the entire
negotiable surface. The largest single one is `GLCanvas3D.cpp` at
+149/-14 (a pick path for
the CAD viewport); everything else is under 60 lines.
One thing about the raw diff: the file count includes everything new,
and the negotiable
surface is the 23 modified files above. Thanks for merging `main` in —
the branch is current
again, and I have kept building on top of it.
The regenerated i18n catalogues (`OrcaSlicer.pot`, `OrcaSlicer_it.po`,
`list.txt`) have been
kept OUT of this branch deliberately — they were 27,314 added lines of
build product standing
between you and the code. They regenerate from source with
`scripts/run_gettext.sh` whenever
you want them refreshed. A Romanian catalogue that had been riding along
was pulled out at
the same time — a translation has no business being reviewed inside a
CAD feature PR.
| | |
|---|---|
| Kernel | OCCT — already linked for STEP import. The dependency delta
is one line: `BUILD_MODULE_ModelingAlgorithms=OFF → ON`. Measured cost
in
[`docs/cad_dependency_weight.md`](https://github.com/tommasobbianchi/Orca-Cad/blob/cad-mainline/docs/CAD/cad_dependency_weight.md)
|
| Constraint solver | vendored SolveSpace `libslvs` subset, 21 files /
~10k lines under `src/libslic3r/slvs/` |
| Build gate | `SLIC3R_CAD` (default ON). With it OFF the tab is not
compiled and the deps prefix matches upstream exactly |
| Persistence | CAD recipe embedded in both the 3MF and BBS-3MF writers
|
| User docs |
[`docs/design_tab.md`](https://github.com/tommasobbianchi/Orca-Cad/blob/cad-mainline/docs/CAD/design_tab.md)
|
| Interaction model | object-driven — point at geometry, it offers the
verbs that apply:
[`docs/cad_ux_guidelines.md`](https://github.com/tommasobbianchi/Orca-Cad/blob/cad-mainline/docs/CAD/cad_ux_guidelines.md)
|
### Why it belongs in the slicer
Every round trip through an external CAD tool costs an export, a
re-import, and the design
intent both steps discard. A part changed after slicing should come back
to its feature
history, not to a mesh. Keeping the model in the slicer preserves that
loop — nozzle
diameter, build volume and material are known at design time. Longer
argument in
[`docs/design_tab_upstream_portability.md`](https://github.com/tommasobbianchi/Orca-Cad/blob/cad-mainline/docs/CAD/design_tab_upstream_portability.md).
### Two things I'd rather you hear from me than find
**Licensing.** The vendored solver is **GPL-3.0**, not LGPL
(`src/libslic3r/slvs/LICENSE`).
The combined work is distributable under AGPL-3.0 and the compatibility
argument is written
out in the portability doc, but this is a project-level decision and I
would like it
confirmed explicitly rather than assumed. If GPL-3.0 in-tree is not
acceptable, the solver
is the separable part — the timeline, features and persistence do not
depend on it.
**One CMake change is larger than it looks.** `CMakeLists.txt` is
+41/-56: it replaces a
hand-maintained list of OCCT DLLs to copy on Windows with a glob plus an
assertion that
every linked toolkit actually has a DLL. The explicit list had already
drifted from what
`libslic3r` links and shipped a portable that died at launch with `error
126`. Happy to
split that out into its own PR if you'd prefer it reviewed separately.
### Not verified
- No automated GUI test. A green kernel run says nothing about the
viewport — synthetic
clicks never drift, so the suite and the UI are two separate realities.
- Card wiring for 9 of the 16 late-wired tools has never been
click-tested.
- The click-test defect rate has not converged: one pass found nothing,
four further days
of work found five more defects. I would not present the quiet pass as
evidence of
stability.
# Screenshots/Recordings/Graphs
One part, start to finish: sketch it, feature it, print it — without
leaving the slicer.
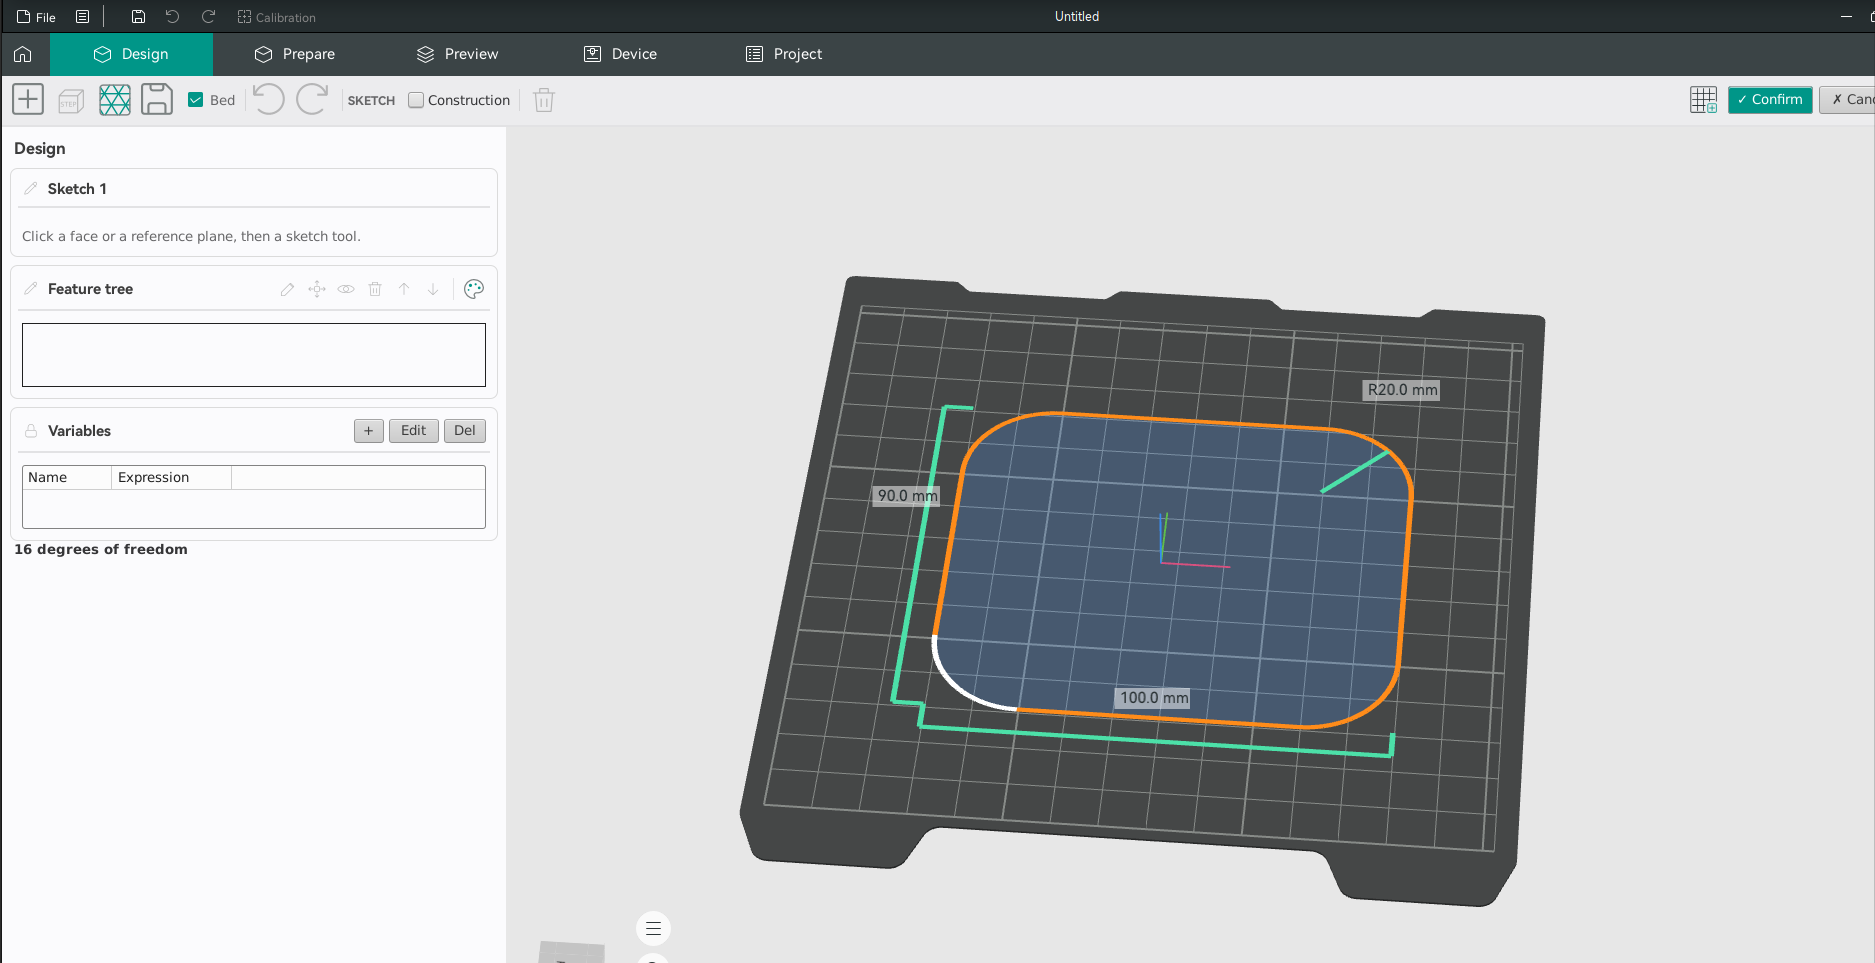
**1. Sketch, constrained and dimensioned.** A 100 × 90 rounded rectangle
drawn straight onto
the bed, R20 corners, live dimensions, and the solver's remaining
degrees of freedom reported
in the panel. The bed is the sketch plane, so the part is sized against
the machine it will be
printed on from the first line.
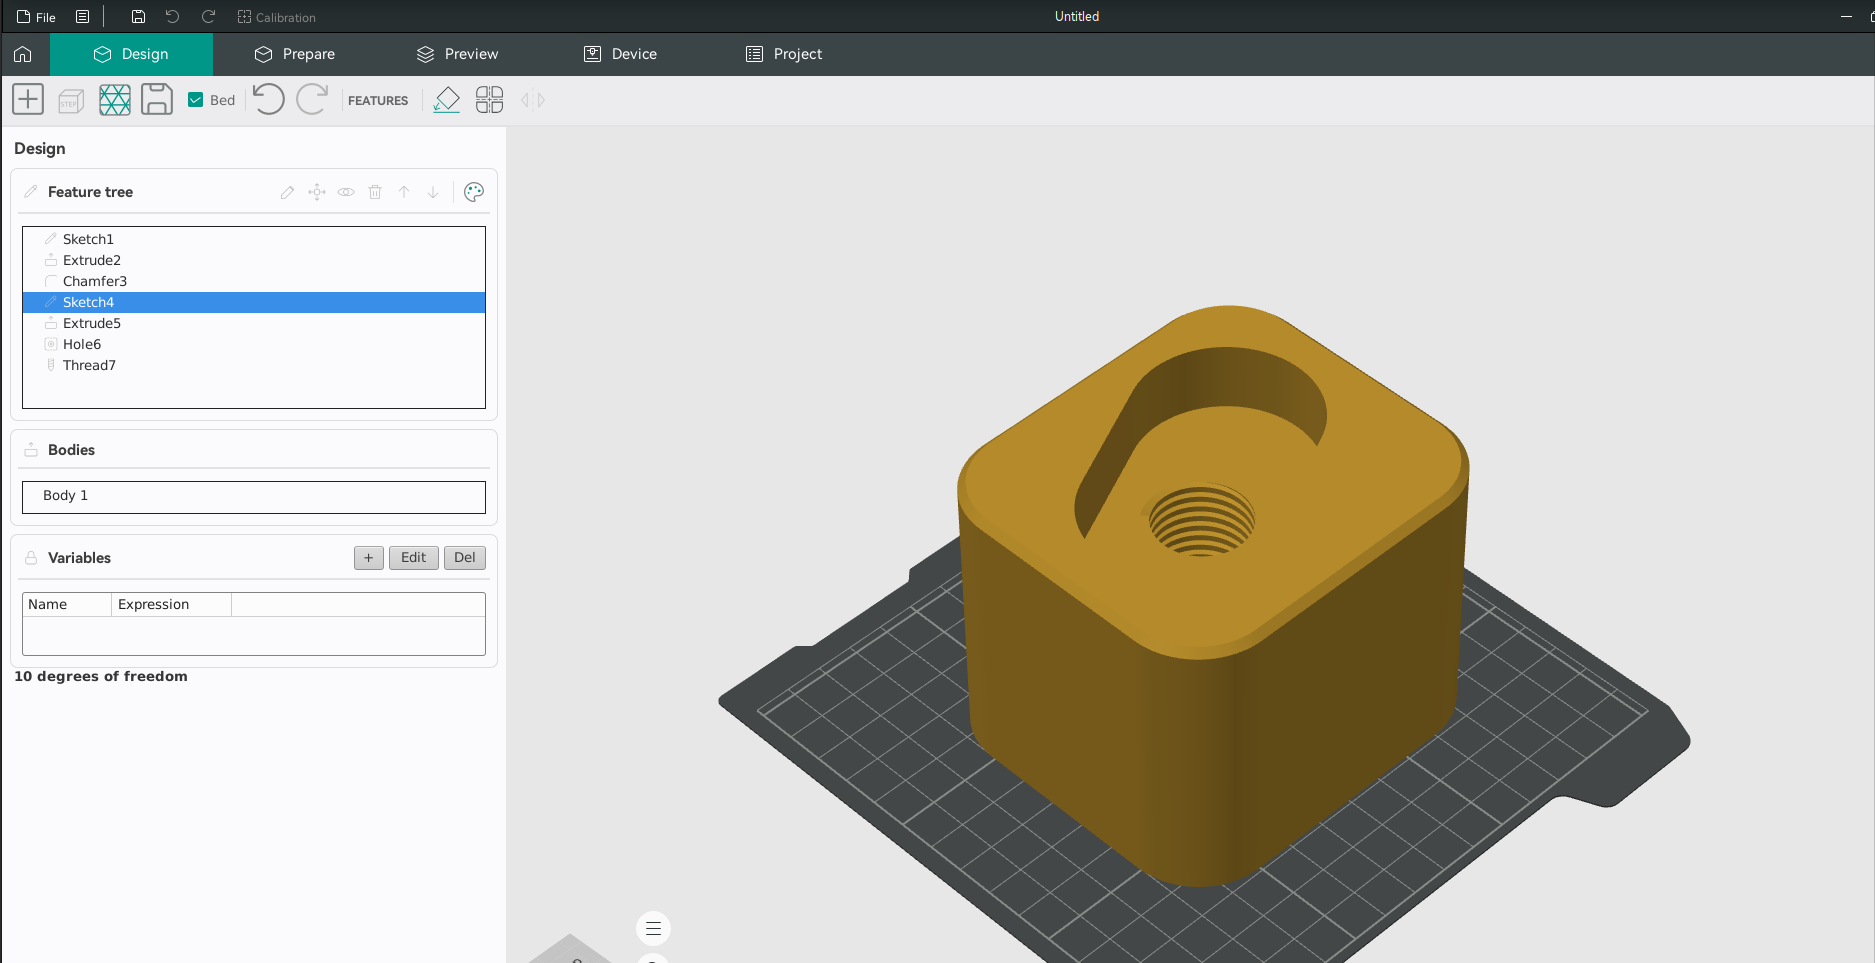
**2. The feature tree is the part.** `Sketch1 → Extrude2 → Chamfer3 →
Sketch4 → Extrude5 →
Hole6 → Thread7`. Every step stays editable and re-evaluates downstream
— the modelled thread
in the boss is a real helical feature, not a texture.
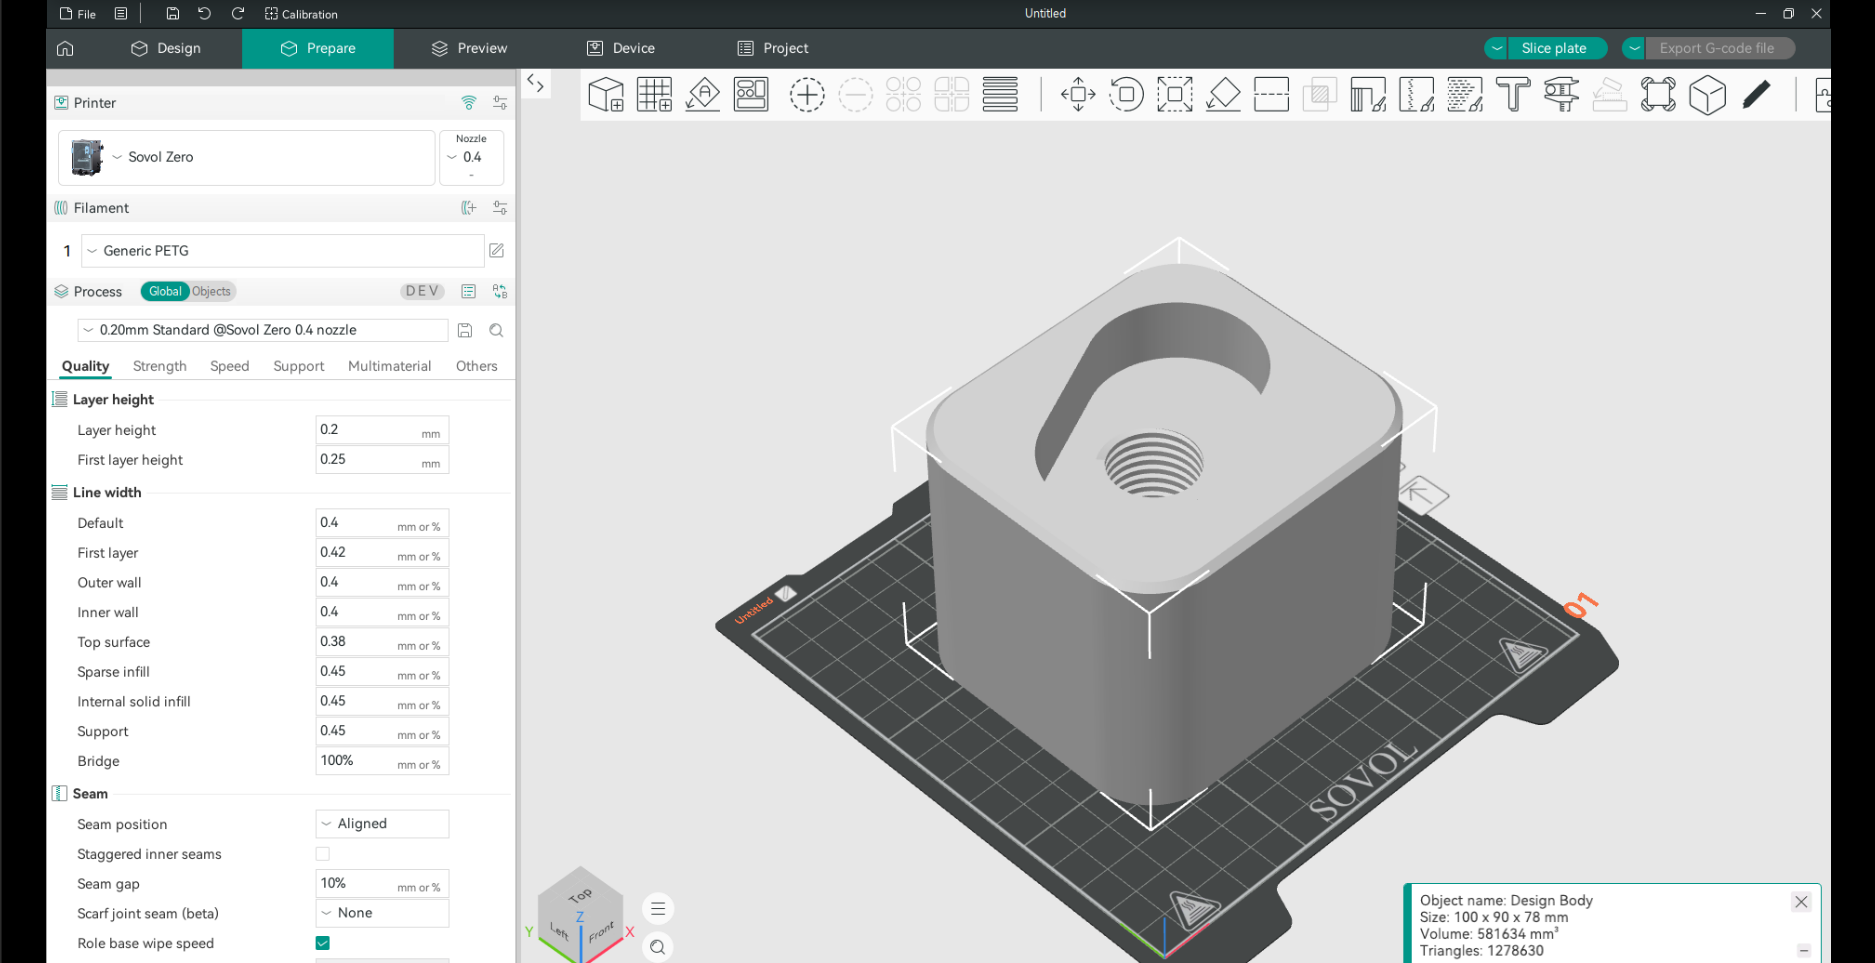
**3. Committed to the plate.** The same body arrives in Prepare as
`Design Body`,
100 × 90 × 78 mm, 581,634 mm³, ready for a Sovol Zero and PETG. No
export, no re-import, no
lost design intent.
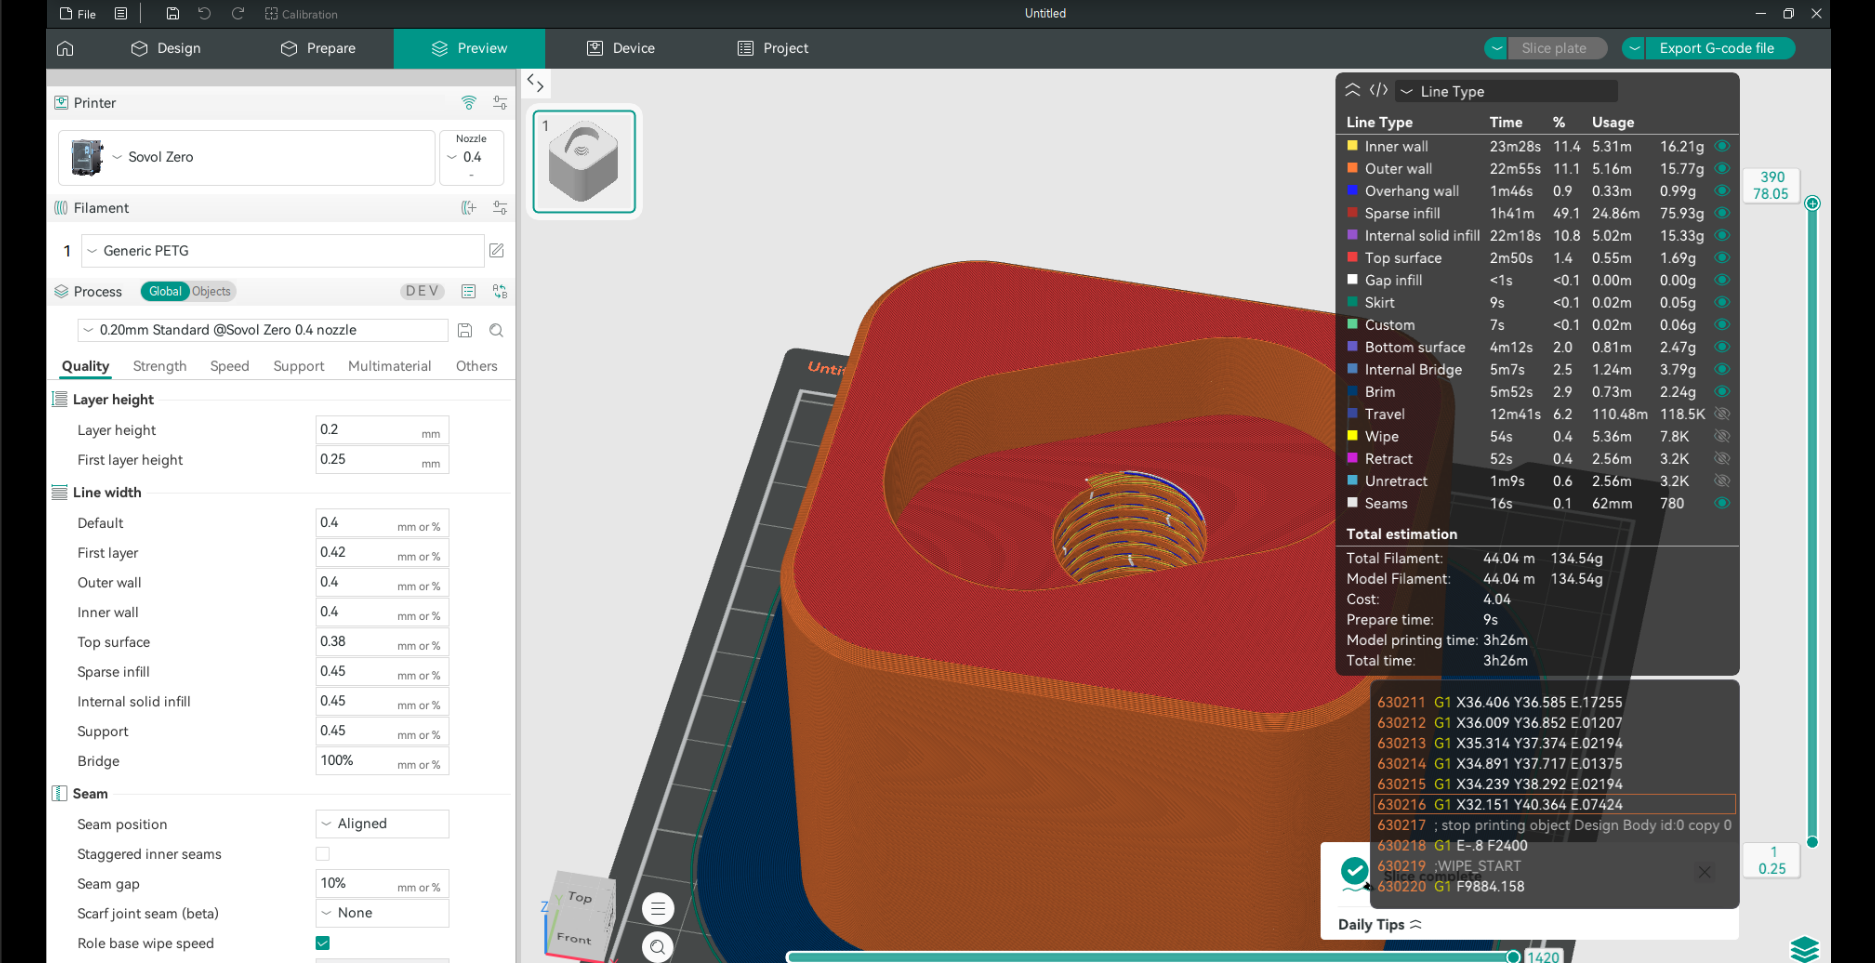
**4. Sliced.** The thread comes out as real helical toolpaths, and the
estimate is 3h26m /
134.54 g. This is the whole argument for the feature in one frame: the
geometry that was
parametric two screens ago is now G-code, and it is still parametric if
you go back.
## Tests
215 `TEST_CASE` blocks across 6 new test files, plus 2 `SCENARIO`s added
to
`tests/libslic3r/test_3mf.cpp` covering the CAD recipe's round trip
through both 3MF
writers. `scripts/kernel-test.sh` is the headless contract: it builds
only
`libslic3r_tests`, needs no display, and exit 0 means the CAD suite
passed.
Happy to slice this differently — kernel + solver first, GUI second — if
that reviews
better for you.
Merged by /bot merge on behalf of @JAYO3D-Official (id 320896770).
Grants: resources/profiles/OrcaFilamentLibrary/filament/JAYO, resources/profiles/OrcaFilamentLibrary.json
Head: fb9a6d70a0
* Run every profile maintenance job from one tool

orca_id_tool.py becomes orca_profile_tool.py, and orca_extra_profile_check.py
and orca_filament_lib.py fold into it as subcommands: check, generate-id, fix,
trim, update-index and update-snapshot. The three scripts already overlapped --
the checker imported half of its rules from the id tool, which in turn kept a
copy-pasted set of output helpers to avoid the resulting import cycle -- while
disagreeing on how a vendor is enumerated, how a JSON file is read and what the
exit code means. One file settles all three.

check, normalize, trim and update-index reproduce their predecessors exactly; normalize and
update-index were diffed byte-for-byte against the old scripts over a copy of
the whole tree. Deliberate changes: the compatible-printers check no longer
switches itself off when --check-materials is passed, an error exits 1 rather
than -1, update-index honours --profile-type and reports a profile it cannot
place instead of dropping it from the index, fix and update-index gained
--dry-run, trim keeps an unindexed file some surviving profile still inherits
from, and vendors are enumerated as directories with an index -- which is why
blacklist.json, a data file that an unscoped index rebuild once wrote four empty
list sections into, loses them here and will not collect them again. The dead
rename_filament_system() helper is gone.

The suite under scripts/tests now covers the maintenance commands too, and CI
runs it; nothing there ran in CI before. No shipped profile data changes apart
from those four keys.

* update vendor index files with "python3 ./scripts/orca_profile_tool.py update-index" and "python3 ./scripts/orca_profile_tool.py normalize"
The U1's heated bed tops out at 100 °C, but these profiles requested
105-110 °C, which leads to print errors unless the user modifies the
printer's firmware configuration.

Affected profiles:
- Snapmaker ABS @U1 base (110/105 → 100)
- Snapmaker ASA @U1 base (110 → 100)
- Fiberon ASA-CF08 @Snapmaker U1 base (105 → 100)
- Fiberon PPS-GF20 @Snapmaker U1 base (105 → 100)

Bumps Snapmaker.json to 02.04.00.10.

Co-authored-by: yw4z <ywsyildiz@gmail.com>
Tiles previously rendered a colored monogram (title/source initials plus an ordinal) with a per-id hue. Show the matching native SVG icon instead:

- AppAction/NativeCommand gain an `icon` field; commands get a curated key->icon table and settings inherit their group header's icon.
- Notebook tracks each page's resource icon name and reports it in tab_options(), so the tab picker can show it too.
- Searcher records the group icon so settings keep it through search.
- Web tile rendering swaps monogramFor/hue for an <img>; drop the now-unused hue/text CSS vars. Add a test asserting every non-empty icon resolves to a shipped SVG.




